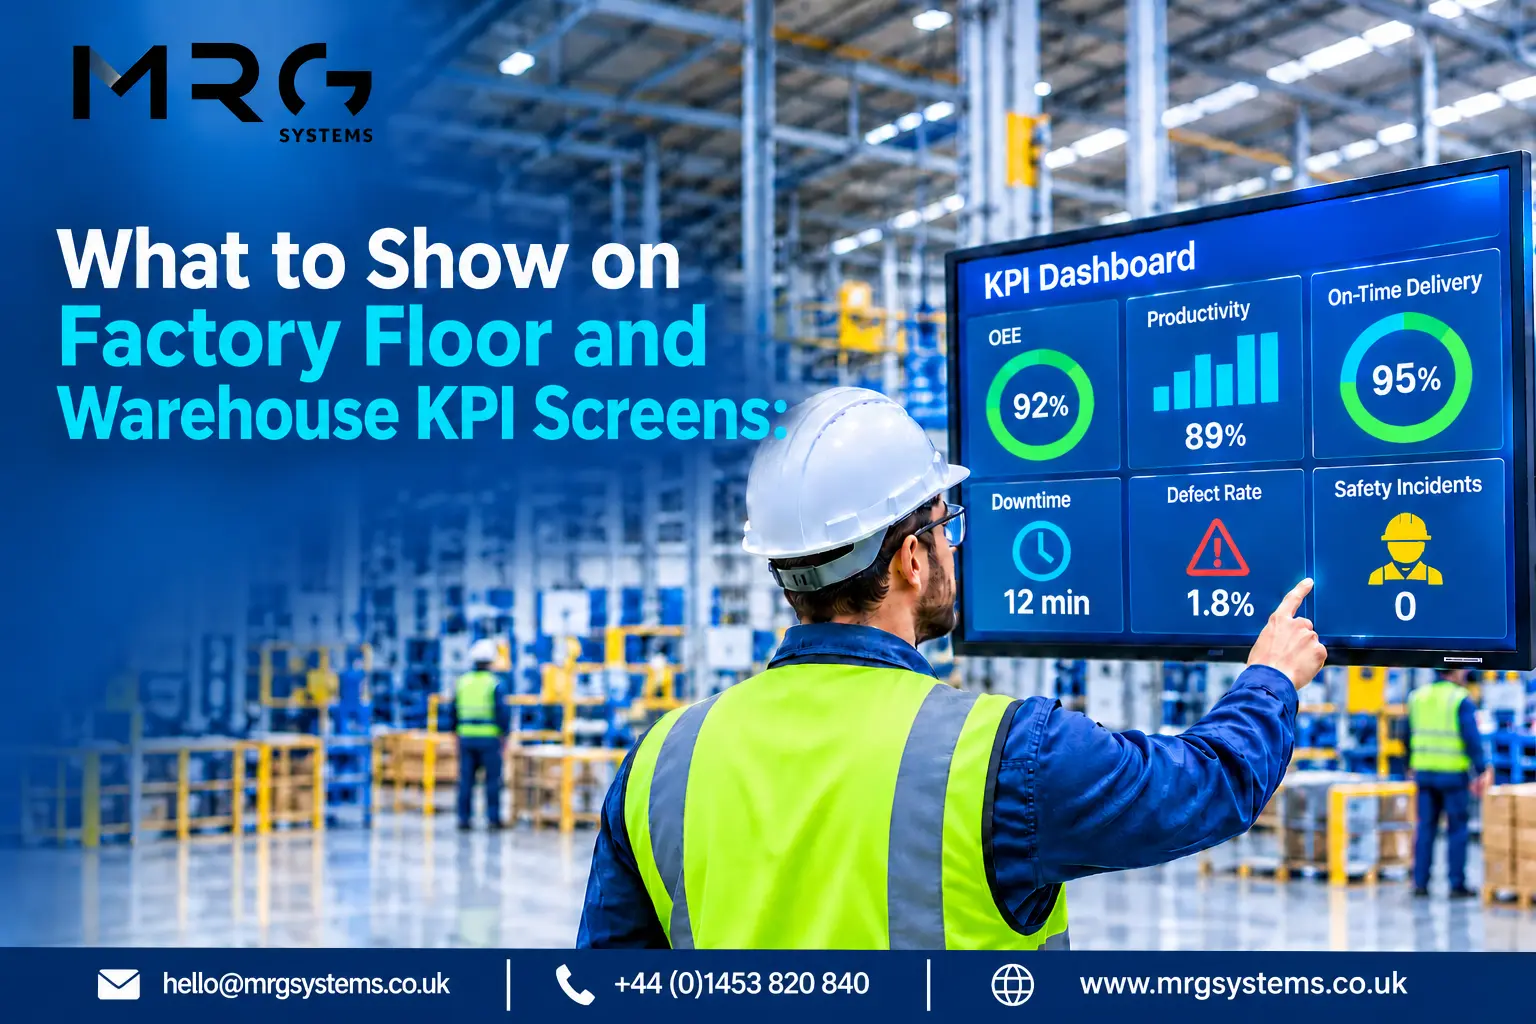
Walk onto most plant floors and you will find a screen above the line that nobody has properly looked at since the week it went in. It is not broken. It shows fourteen numbers, refreshed every fifteen minutes, with a target beside none of them. The operator read it carefully for about four days, worked out that nothing on it told her anything she could change before the end of her shift, and stopped looking.
That is the problem with most factory floor digital signage, and it is not a hardware problem. Good digital signage software will display anything you point it at, which is precisely why the choice of what to point it at matters so much.
| The short answer The metrics that change behaviour on a factory or warehouse screen are: output against a pace adjusted target, OEE split into its three parts, ranked downtime causes, changeover time against standard, cycle time against plan, short stop count, first pass yield, scrap and rework in money, open quality holds, picks per hour against plan, pick accuracy, dock to stock time, dispatch progress against the daily cut off, open safety actions, and shift skills cover.Show five to eight on any one screen, choose them for the person standing in front of it, and put a target beside every number. A metric with no target is trivia. |
The case for visible metrics is not a marketing claim. Locke and Latham found consistently that specific, demanding goals beat vague encouragement, and that the effect depends on feedback. Remove the target and you have feedback with no reference point. Remove the live number and you have a goal with no feedback.
Attention also habituates. A number that does not change, or that nobody present can influence, drops out of awareness within a fortnight. And a metric naming an individual invites concealment rather than problem solving, because the quickest route to a better looking number is to stop recording inconvenient events. Measure the line, the cell or the shift. Any digital signage software that encourages per operator leaderboards is solving the wrong problem.
Before a metric goes on a screen, run it through four questions. This removes about half of what clients originally ask for.
Fail any one and it belongs in a weekly report. The strongest digital signage solutions we have built are the ones where the client cut the original list in half. Our four step process starts with that conversation rather than with hardware.
| Not sure which of your current metrics would survive that test? Fill in the enquiry form on our contact page or call us on +44 (0)1453 820 840. Send us your screen layout and we will tell you which numbers we would keep. |
| Metric | Who acts on it | Refresh | Most common mistake |
| 1. Output against pace adjusted target | Operator, line lead | 1 to 5 min | Using the flat shift total, so it only becomes useful too late to act |
| 2. OEE, split three ways | Line lead, supervisor | 5 to 15 min | A single figure that hides which of the three parts failed |
| 3. Downtime by cause, ranked | Operator, maintenance | Live | A cause list so long that nothing stands out |
| 4. Changeover against standard | Changeover team | Live | One generic standard for every changeover |
| Cycle time against time taken | Cell operators | Every cycle | A shift average that flattens the variation |
| 6. Short stop count | Operator, maintenance | Live | Counting stops without showing the duration band |
| 7. First pass yield | Operator, quality | 15 to 30 min | Reporting final yield after rework and calling it first pass |
| 8. Scrap and rework in money | Supervisor, operator | 15 to 30 min | A fully loaded cost that finance will dispute |
| 9. Open quality holds | Quality, planning | Live | Showing the count without the ageing |
| 10. Picks per hour against plan | Pickers, team leader | 15 min | Aggregating zones, which hides the aisle causing the backlog |
| 11. Pick accuracy per 1,000 lines | Pickers, team leader | Hourly | Showing the rate without the volume |
| 12. Dock to stock time | Goods in team | Hourly | The average alone, hiding the pallet stuck since Tuesday |
| 13. Dispatch against daily cut off | Whole dispatch floor | Live | Starting the countdown too late to redeploy labour |
| 14. Open safety actions and near misses | Supervisor, safety lead | Daily | Treating a falling near miss count as good news |
| 15. Shift skills cover by role | Supervisor | Shift start | Listing names rather than roles |
Table 1. The fifteen metrics, who acts on each, and the mistake that neutralises it.
Three of these need a word of explanation, because they are where most digital signage solutions are set up wrongly.
Output needs a pace adjusted target. A shift target of 1,500 units tells an operator nothing at 09:40. A target that moves with the clock, showing 340 against an expected 365, tells her she is an hour behind with time to recover.
Warehouse metrics belong on screens too, and almost every guide to this subject stops at the production line. Picks per hour by zone, pick accuracy, dock to stock and a live dispatch countdown all respond strongly to visibility, because the deadline is real and shared. Good operational intelligence software pulls these straight from the warehouse management system, so nobody rekeys anything. Our pages on warehouse digital signage and transport and logistics cover how those feeds connect.
Days since last incident is the wrong safety metric for a live screen. It is purely lagging, nobody can influence it through action, and it risks suppressing reporting because an incident resets a number the whole site is watching. Show open safety actions with their ageing instead. The Health and Safety Executive recorded 126 worker deaths in Great Britain in 2025/26 provisionally, 18 in manufacturing and 15 in transportation and storage. A safety screen should drive action, not celebrate a streak.
| OEE benchmark | Figure | What it means for your screen target |
| Median plant | 60% | Where most lines actually sit once losses are measured honestly |
| Top quartile | 75% | A realistic stretch target for a line that is already measured |
| World class reference | 85% | A discrete assembly reference point, not a universal goal |
Table 2. OEE benchmark distribution. Source: TeepTrak 2026 Manufacturing OEE Benchmark Report, direct sensor data from 450 plants across 30 countries.
That 85 percent figure is the most misquoted number in manufacturing. It comes from Nakajima’s total productive maintenance work and describes high volume discrete assembly. Applied to a pharmaceutical line with validated cleaning cycles it sets a target the process cannot reach, and a target nobody believes is worse than none.
| Sector | Median OEE | Top decile OEE |
| Metals and heavy industry | 71% | 88% |
| Pharmaceutical | 52% | 76% |
| Aerospace components | 48% | 72% |
Table 3. Sector median and top decile OEE. Set the screen target against your own sector and your own trend, not against a single published figure.
One more caution before OEE goes near a screen. The same benchmark found that plants moving from paper logs to direct sensor measurement typically uncover five to fifteen percentage points of previously invisible losses. If your current figure comes from a clipboard, expect the number to drop when operational intelligence software starts measuring it properly. Say so before go live, not after.
| Decision the screen supports | Sensible refresh | What goes wrong otherwise |
| Stop or escalate now | Live, under 30 seconds | The event is over before the screen shows it |
| Catch up within the hour | 1 to 5 minutes | Recovery time lost to a stale number |
| Adjust within the shift | 15 to 30 minutes | A twitchy number reads as noise and gets ignored |
| Plan the next shift | Once per shift | Constant movement implies urgency that is not there |
| Review the week | Daily or weekly | Belongs in a report, not on a floor screen |
Table 4. Match the interval to the decision. This is the setting most often left on a default.
A screen showing stale data without saying so is worse than a blank one, because people act on it. Any serious operational intelligence software should display data age or grey the panel when a feed stops, and you should test that by pulling the feed before go live. That principle sits behind our visual intelligence approach: the right information at the right moment, not more information.
Readability is where otherwise sound digital signage solutions quietly lose their value, because the layout gets approved on a laptop and then hung twelve metres from the nearest operator.
Factory floor digital signage rarely fails loudly. It fails quietly, in one of these seven ways.
The sixth is the quiet killer. Every screen needs a named owner, a monthly check that the feed is live and reconciles to source, and a quarterly review of the metric set. No digital signage software can do that part for you.
| Want a second opinion on an existing screen estate? Fill in the enquiry form on our contact page or call us on +44 (0)1453 820 840. Send a photograph of one screen and we will come back with what we would change. |
Pick one line. Baseline for four weeks, recording response time from a stop starting to someone arriving at the machine, because that is the behaviour the screen is meant to change. Install one screen with one owned metric set and run six weeks, changing nothing else. Compare response time, downtime minutes and first pass yield against the baseline and against a comparable line with no screen. That comparison line separates a result from a coincidence.
Be honest about the limits. The test shows whether response behaviour changed on that line. It does not isolate the screen from the attention any new initiative brings, and an internal result that admits that survives scrutiny far better than one claiming too much.
What KPIs should a factory display on digital signage? Output against a pace adjusted target, OEE split into availability, performance and quality, ranked downtime causes, changeover time against standard, cycle time against takt, short stops, first pass yield, scrap in money and open quality holds. Choose five to eight per screen based on who stands in front of it.
How often should factory KPI screens refresh? Match the interval to the decision: live for escalation, one to five minutes for recovery inside the hour, fifteen to thirty minutes for within shift adjustment, once per shift for planning.
What should warehouse digital signage show that a factory screen does not? Picks per hour against the planned rate for that hour by zone, pick accuracy per thousand lines, dock to stock time with the oldest outstanding consignment, and a live countdown against the carrier cut off.
Can digital signage software connect to our MES or ERP? Yes. Mature operational intelligence software connects to MES, ERP, warehouse management and BI feeds and refreshes without anyone updating a slide. Integration is rarely the hard part. Deciding which five numbers deserve the wall is.
What is the difference between a floor screen and a manager dashboard? A dashboard supports analysis and allows filtering and drill down. A floor screen supports a decision in the next few minutes by someone standing up who will never interact with it. Pointing digital signage software at an existing management dashboard is the most common way a screen programme fails.
Start with one line, one audience and five metrics that pass the four question test. Give the screen an owner and baseline before you install. We have been building visual systems for British industry since 1983, from our base in Stonehouse, and the pattern has not changed much: the plants that get value from digital signage solutions decided what the screen was for before deciding where it would hang. That is as true of manufacturing digital signage today as it was of the printed boards it replaced. There is more on this in our pieces on manufacturing digital signage and shopfloor to boardroom visibility.
| Tell us about the line or zone you would start with. Fill in the enquiry form on our contact page or call us on +44 (0)1453 820 840. We will come back with a suggested metric set, refresh intervals and a measurement plan for a ten week trial. |